Belt conveyors in mining parts,

Belt conveyors in mining: parts, loads and the places where they fail

The US Mine Safety and Health Administration (MSHA) describes conveyor systems as an important way to move material at surface and underground mines, from a single belt to a series of belts spanning miles [1]. It also states that all conveyor systems have inherent dangers while in motion [1]. Most discussion of belt condition starts at the belt itself, but a conveyor is a set of parts that load one another, and both damage and injury cluster at particular points. This article walks through those parts, what sets the forces in the belt, and where problems concentrate. Figure 1 shows the layout used throughout.

A belt conveyor carries material on a belt that runs in a closed loop. Jurdziak and colleagues note that belts are assembled into a closed loop from several sections, which arrive at the installation site on reels [2]. The loop turns around pulleys. Guidance from the Ontario Ministry of Labour, Immigration, Training and Skills Development names the head, tail, drive, deflection and tension pulleys, and the carry and return rollers [3]. In a gravity take-up, which provides tension for the belt, a free weight hangs on a tension pulley from deflection (bend) pulleys on the return side of the belt [3].
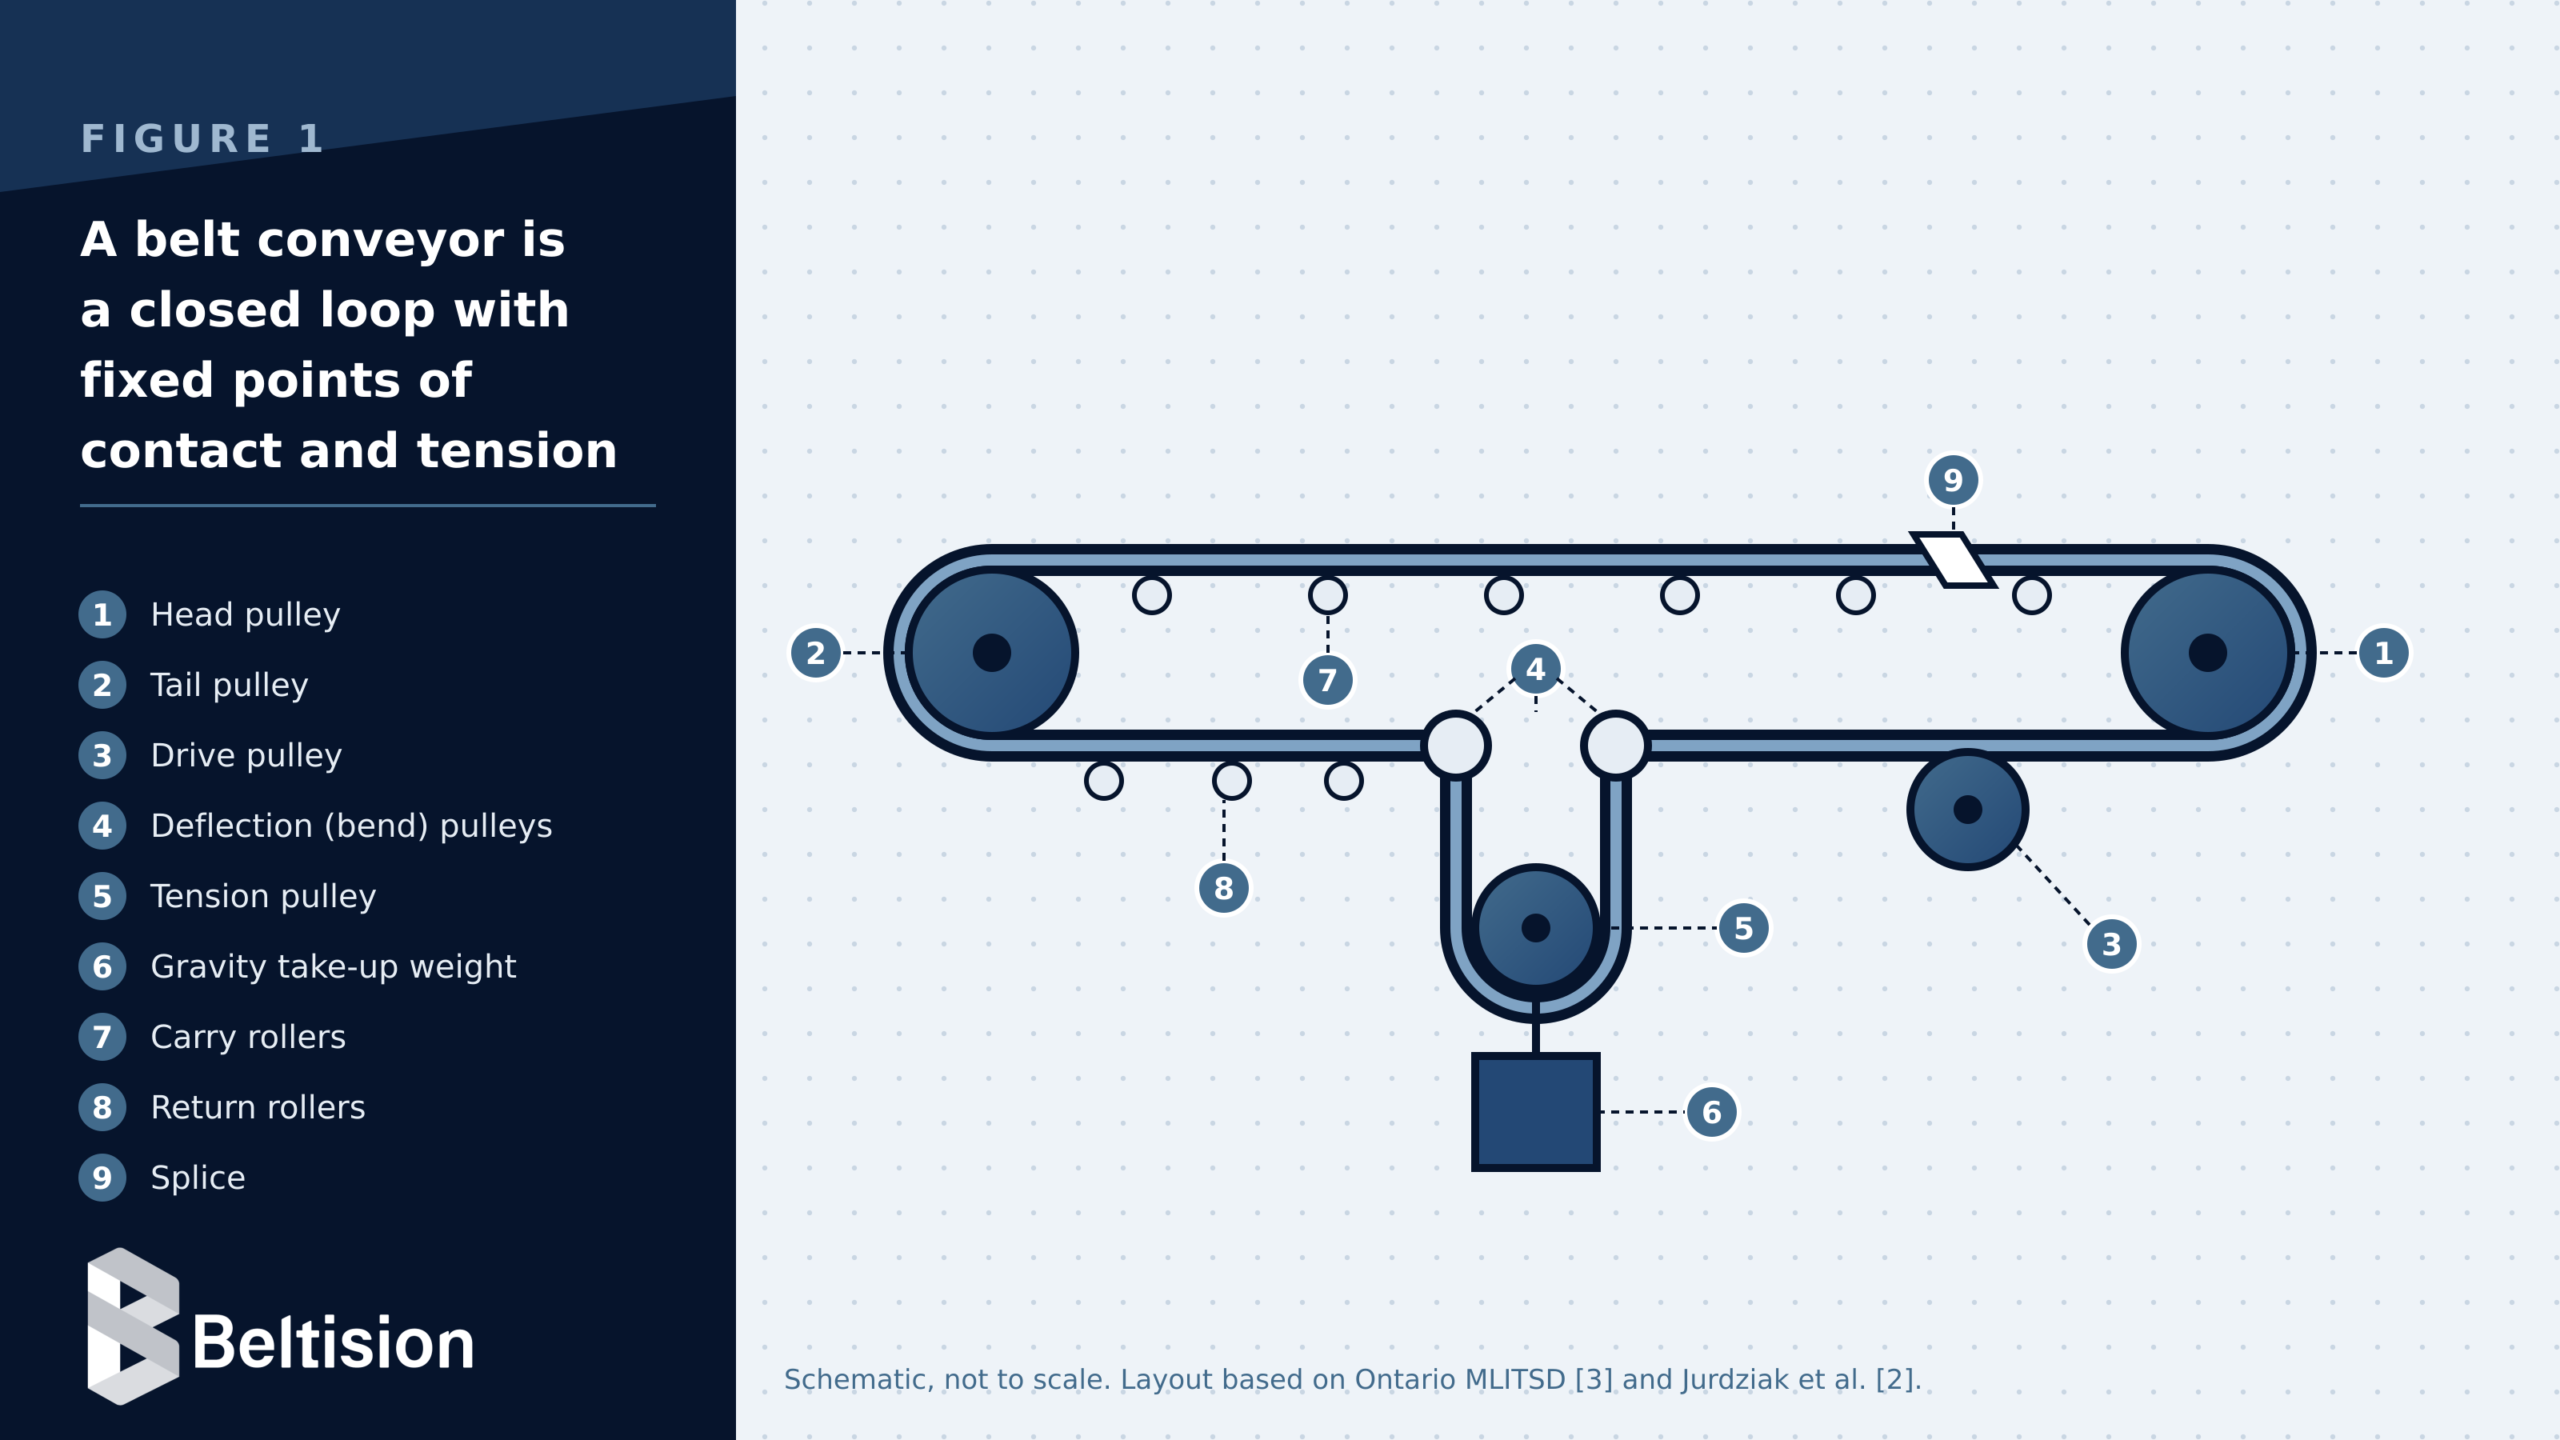
Schematic of a belt conveyor loop showing head, tail, drive, deflection and tension pulleys, carry and return rollers, a gravity take-up and a splice
Figure 1. Original explanatory diagram of a belt conveyor loop with the parts named in Ontario guidance [3] and a splice [2]. Numbers refer to the legend in the figure. Schematic, not to scale; the positions of the drive pulley, rollers and take-up are illustrative.

The belt itself has a layered structure. A review of non-destructive testing for conveyor belts describes rubber cover layers and load-bearing elements, which are fabric plies or steel cord reinforcement [4]. Jurdziak and colleagues classify belts as textile-reinforced or steel cord-reinforced according to the core material, and describe the core as the layer that transmits the longitudinal forces needed to move large masses of material [2]. Textile-reinforced belts may be joined by hot vulcanization, cold bonding or welding, or mechanical fasteners; steel cord belts are joined only by hot vulcanized splices [2].

A splice is the joint that closes the loop, and the belt core loses its continuity over a short region there [2]. For that reason Jurdziak and colleagues describe the splice as the weakest link in the loop [2]. They report that splices are susceptible to damage and irregularities arising from assembly errors, improper vulcanization parameters or unfavourable operating conditions [2].

International standard ISO 5048 covers the forces that load this loop. According to its published scope, it specifies methods for calculating the operating power needed at the driving pulley and the tensile forces in the belt of conveyors with carrying idlers. It also defines terms, symbols and units, the resistances to motion, the driving force and power requirements, and the capacity and cross-section of a conveyor with a smooth patternless belt [5]. The 1989 edition was last reviewed and confirmed in 2026, and ISO lists it as current [5]. This article uses only the scope text, which is public; the formulas and values are in the full standard and are not reproduced here.

The same review lists the common failures: surface wear, cuts, longitudinal tears, delamination of cover layers, damage to the steel cord core and local overheating caused by friction [4]. Surface wear is the most common type of damage and results from contact between the belt and the conveyed material [4]. Cuts and tears are typically sudden and severe, and often mean replacing a whole section of belt [4]. Fracture or corrosion of steel cords reduces tensile strength [4]. The authors name sharp foreign objects, structural misalignment, local overstressing and splice defects as root causes of sudden failures [4]. A separate article in this series covers the damage types and their causes in detail.

The parts that load the belt are also the places where people get caught. Ontario guidance says accessible pinch points must be guarded at the head, tail, drive, deflection and tension pulleys, and at the return and carry rollers where the lift of the belt is restricted; guards generally extend at least 0.9 metres from the pinch point unless they make it inaccessible [3]. MSHA reports that fatal accidents related to working near, inspecting, adjusting or maintaining conveyor belts occur each year at underground and surface mines [1]. Its key practices include locking out and tagging out energy at the source during maintenance, guarding moving parts including rollers and the head and tail areas, and installing pull cords for emergency stops [1]. The Ontario guidance states that it does not replace the Occupational Health and Safety Act or its regulations and is not legal advice [3]. Two companion articles in this series cover safety practice and Ontario’s mining regulation.

Any conveyor can be read with a few plain questions. Where are the splices, and how were they made and inspected? Which pinch points can be reached, and are the guards in place at the distances the rules ask for? What do the maintenance records say about wear, cuts and overheating, and where on the loop were they found? Which calculation sets the drive power and belt tension, and where is it documented?

References

  1. Mine Safety and Health Administration. Safety topic: conveyor systems [Internet]. Arlington (VA): U.S. Department of Labor; [cited 2026 Nov 10]. Available from: https://www.msha.gov/node/232931
  2. Jurdziak L, Błażej R, Rzeszowska A. Non-destructive diagnostics in the assessment of splice geometry in steel cord conveyor belts. Appl Sci. 2025;15(9):5034. doi:10.3390/app15095034. Available from: https://doi.org/10.3390/app15095034
  3. Ontario Ministry of Labour, Immigration, Training and Skills Development. Conveyor guarding in mines [Internet]. Toronto: Government of Ontario; updated 2024 Nov 7 [cited 2026 Nov 10]. Available from: https://www.ontario.ca/page/conveyor-guarding-mines
  4. Rzeszowska A, Błażej R, Jurdziak L. Non-destructive testing for conveyor belt monitoring and diagnostics: a review. Appl Sci. 2025;15(24):13272. doi:10.3390/app152413272. Available from: https://doi.org/10.3390/app152413272
  5. International Organization for Standardization. ISO 5048:1989 Continuous mechanical handling equipment. Belt conveyors with carrying idlers. Calculation of operating power and tensile forces [Internet]. Geneva: ISO; 1989 [reviewed and confirmed 2026; cited 2026 Nov 10]. Available from: https://www.iso.org/standard/11069.html
How Predictive Maintenance is Reducing Downtime in Conveyor Belt Operations

How Predictive Maintenance is Reducing Downtime in Conveyor Belt Operations

How Predictive Maintenance is Reducing Downtime in Conveyor Belt Operations

In industries where every minute of equipment downtime translates into lost productivity and revenue, maintenance strategies have become a critical area of innovation. Nowhere is this more evident than in conveyor belt operations, especially in mining, manufacturing, and logistics sectors. These systems operate under constant load and environmental stress, making failure both frequent and costly.

Predictive maintenance, powered by AI and the Internet of Things (IoT), is emerging as a
game-changer. It helps operators anticipate mechanical issues before they occur, reducing unplanned downtime by up to 40% and cutting maintenance costs by nearly 30% in some industries. This article explores how this proactive approach is transforming conveyor belt reliability, with insights drawn from leading academic research.


From Breakdown to Prediction: The Shift in Maintenance Culture

Historically, companies relied on two primary maintenance strategies:

  • Reactive Maintenance (run-to-failure): Wait for equipment to break before fixing it
  • Preventive Maintenance: Schedule servicing at regular intervals, regardless of actual need

While preventive maintenance is better than waiting for failure, it’s still inefficient. Equipment that doesn’t need repair gets unnecessary attention, while hidden faults can still go unnoticed.

Predictive Maintenance (PdM) changes the game. Instead of depending on fixed schedules, it uses real-time condition monitoring and data analytics to determine when maintenance is actually needed. In other words, maintenance happens only when risk is high, not too soon, not too late.


How Predictive Maintenance Works

The core of predictive maintenance lies in two enablers:

  1. IoT Sensors: Continuously collect real-time data on vibration, temperature, load, and belt alignment
  2. Machine Learning Algorithms: Analyze historical and live data to detect anomalies and predict failures

Together, these technologies enable condition-based maintenance, meaning actions are based on the actual health of the equipment, not a calendar.

For conveyor belts, PdM systems can identify early signs of:

  • Belt slippage or misalignment
  • Abnormal motor vibrations
  • Surface wear or tear
  • Tension irregularities


Machine Learning at the Core of Prediction

Machine learning (ML) algorithms are the brain behind predictive systems. Depending on the type of data and use case, several models are used:

  • Classification algorithms (like decision trees, support vector machines): Determine whether a component is “healthy” or needs maintenance
  • Regression models: Estimate Remaining Useful Life (RUL) of components
  • Anomaly detection: Spot deviations from normal operating patterns without labeled data
  • Reinforcement learning: Continuously improve scheduling decisions over time

In recent case studies, ML models have achieved:

  • 90–95% prediction accuracy with decision trees and random forest classifiers
  • Early detection of degradation via anomaly detection methods
  • Dynamic optimization of maintenance intervals through reinforcement learning

These outcomes result in fewer false alarms, smarter repairs, and greater trust in the system’s insights.


The Role of IoT: Real-Time Data for Real-Time Decisions

IoT sensors are embedded throughout conveyor systems to capture physical parameters such as:

  • Vibration patterns
  • Temperature spikes
  • Belt tension and alignment
  • Pressure and motor load

This data is transmitted over secure networks to cloud or edge computing platforms, where machine learning models analyze it in real time.

A multi-layered IoT architecture enables:

  • Edge computing for fast, local analysis
  • Cloud integration for historical data storage and model training
  • User dashboards that visualize equipment status and alerts

The result is a continuous feedback loop between machine performance, prediction models, and maintenance teams.


Downtime Reduction: Real Numbers, Real Impact

The impact of predictive maintenance on downtime reduction is well-documented:

  • Companies using PdM report up to 40% less unplanned downtime
  • Conveyor belt systems benefit most from early failure detection of motors, rollers, and belts
  • Maintenance can be scheduled during low-demand hours, minimizing production loss

For example, in the railway sector, Deutsche Bahn used predictive analytics to detect anomalies in braking systems and avoid train delays. Similarly, manufacturers like GE and Siemens reduced failures in turbines and motors by continuously analyzing sensor data.

In mining, where conveyor belts can run for kilometers and are often in remote or underground locations, PdM helps avoid the high cost of emergency service calls and idle machinery.


Financial Gains: Lower Costs, Higher ROI

Beyond operational uptime, predictive maintenance drives significant cost savings:


Metric

Before PdM

After PdM

Change

Maintenance costs

$500,000

$350,000

↓ 30%

Annual unplanned downtime hours

1000 hrs

600 hrs

↓ 40%

ROI payback period

–

6–18 months

Fast recovery

This performance is especially important in industries where even an hour of downtime can cost thousands or millions of dollars.


Scalable and Flexible for Industrial Applications

One of PdM’s greatest strengths is scalability. Systems can be deployed across:

  • Large manufacturing plants with multiple conveyor lines
  • Mining operations with rugged terrain and remote sites
  • Logistics hubs needing high throughput and precision

Additionally, PdM frameworks can be adapted to:

  • New conveyor models and equipment types
  • Legacy systems (via retrofitted sensors)
  • Various network conditions (Wi-Fi, LoRa, Zigbee)

Even better, cloud-based platforms enable cross-site insights, helping companies standardize best practices across multiple facilities.


Challenges to Overcome

Like any transformation, predictive maintenance does come with hurdles:

  • Initial investment in IoT infrastructure and analytics platforms
  • Integration complexity with existing maintenance workflows
  • Dependence on data quality — inaccurate or sparse data leads to poor predictions
  • Skills gap — teams may need training in analytics or AI tools

However, the long-term return, in reduced costs, extended equipment life, and improved safety, far outweighs the upfront effort.


Conclusion: Smarter Maintenance, Stronger Performance

Predictive maintenance is more than a tech upgrade, it’s a strategic shift that empowers industrial operations to work smarter, not harder.

For conveyor belt systems, especially in high-demand sectors like mining and manufacturing, PdM:

  • Prevents unexpected failures
  • Cuts downtime dramatically
  • Extends equipment lifespan
  • Unlocks better resource planning

Backed by machine learning and IoT, predictive systems are helping industries transition from reactive firefighting to proactive precision. As adoption spreads, the competitive advantage will go to companies who embrace these innovations early.


Source Acknowledgment

This article is informed by insights from the following academic sources:

  1. Patil, Dimple. Artificial Intelligence-Driven Predictive Maintenance in Manufacturing: Enhancing Operational Efficiency, Minimizing Downtime, and Optimizing Resource Utilization (December 11, 2024).
    Available at SSRN: https://ssrn.com/abstract=5057406 or http://dx.doi.org/10.2139/ssrn.5057406

Ahuja, Ashutosh & Gupta, Mandakini. Optimizing Predictive Maintenance with Machine Learning and IoT: A Business Strategy for Reducing Downtime and Operational Costs (October 7, 2024).
DOI: 10.13140/RG.2.2.15574.46400
Available at SSRN: https://ssrn.com/abstract=4994457

Applications of Artificial Intelligence for Smart Conveyor Belt Monitoring Systems

Applications of Artificial Intelligence for Smart Conveyor Belt Monitoring Systems

Applications of Artificial Intelligence for Smart Conveyor Belt Monitoring Systems

In the industrial world, conveyor belts are the lifeblood of production lines, mining sites, and logistics networks. Yet, behind their mechanical simplicity lies a complex reality: wear, misalignment, and mechanical failures can cause major delays, safety hazards, and financial losses.

That’s where artificial intelligence (AI) steps in.

AI-powered monitoring systems are reshaping how industries oversee and maintain conveyor belts, bringing predictive insights, real-time alerts, and operational optimization to the heart of material handling. This article explores how technologies like machine learning, computer vision, and IoT are redefining conveyor belt performance, especially in high-demand sectors like mining and manufacturing.

Why Conveyor Belts Need Smarter Monitoring

Conveyor belts are used to transport everything from ore to boxes, operating continuously in high-stress environments. Traditionally, maintenance has relied on manual inspections and scheduled checkups. But these approaches can’t always detect small problems before they escalate into major failures.

For industries where uptime equals revenue (like mining or large-scale manufacturing) waiting for something to break is simply too risky.

AI enables proactive monitoring, turning reactive systems into intelligent, self-learning infrastructures. With AI, conveyor belts can now detect early signs of failure, alert maintenance teams, and even suggest optimized operating parameters.

Key AI Technologies in Smart Conveyor Monitoring

Modern AI systems don’t rely on a single technology, they combine machine learning, computer vision, and the Internet of Things (IoT) to monitor belt health, analyze system data, and drive predictive maintenance strategies.

  1. Machine Learning (ML)

Machine learning algorithms use historical and real-time data to detect anomalies and forecast failures. These models learn from patterns in temperature, vibration, speed, and load data.

  • Neural networks can identify subtle changes in sensor data that indicate belt wear or impending failure.
  • Support Vector Machines (SVM) classify operational states as normal or faulty based on sensor inputs.
  • Decision trees help maintenance teams understand root causes by mapping system conditions to potential faults.

These models evolve over time, becoming more accurate as they analyze more operational data.

  1. Computer Vision (CV)

Computer vision systems use high-resolution cameras and deep learning algorithms (like CNNs) to inspect conveyor belts in real time.

They can:

  • Detect surface tears, fraying, or misalignment.
  • Track belt movement for deviation or tension issues.
  • Monitor material flow for consistency and safety.

CV is especially useful in environments where human inspection is limited or unsafe, like underground mining operations or high-speed assembly lines.

  1. Internet of Things (IoT)

IoT sensors form the backbone of AI-based monitoring systems. These sensors continuously measure key parameters such as:

  • Vibration levels
  • Motor temperature
  • Belt tension
  • Speed and alignment

This real-time data is streamed to cloud or edge computing systems where AI models process the input, identify risks, and trigger alerts.

IoT integration enables 24/7 monitoring of multiple conveyor lines with centralized dashboards for operators.

Real-World Benefits for Industry Stakeholders

Industries that adopt AI-driven conveyor monitoring systems benefit in several critical ways:

  • Reduced downtime: Predictive maintenance minimizes unplanned stops and keeps operations running.
  • Increased equipment lifespan: Early intervention prevents minor issues from causing major damage.
  • Improved safety: Real-time alerts help prevent accidents caused by mechanical failure.
  • Cost savings: Optimized maintenance schedules reduce labor costs and avoid emergency repairs.
  • Higher productivity: Continuous flow of materials ensures consistent output and revenue.

These advantages are particularly relevant in mining, where conveyor belts operate under extreme conditions and failures can halt entire production lines.

Predictive Maintenance in Action

Predictive maintenance is one of the most impactful applications of AI in conveyor monitoring.

Instead of fixing components after failure, AI models predict when maintenance will be needed, allowing teams to plan ahead.

These systems:

  • Analyze historical trends and current data
  • Estimate the remaining useful life (RUL) of key parts
  • Recommend optimal maintenance intervals

By implementing predictive maintenance, companies not only reduce downtime but also extend the life of their equipment and improve overall reliability.

Optimization Through AI

AI doesn’t just detect problems, it also improves performance.

Machine learning models can:

  • Adjust belt speed based on load
  • Distribute materials more evenly
  • Reduce energy consumption
  • Adapt to environmental conditions in real time

Some systems even integrate adaptive control loops, automatically tuning belt tension or load distribution to optimize efficiency.

This level of system intelligence enables facilities to operate at peak performance while minimizing environmental and energy costs.

Challenges and the Road Ahead

Despite the clear benefits, AI-based conveyor monitoring systems face some implementation hurdles:

  • Data quality: Inconsistent or noisy sensor data can reduce model accuracy.
  • Model transparency: Deep learning models can be difficult to interpret, which can hinder trust among engineers.
  • Scalability: AI solutions must adapt to varying conveyor setups across multiple facilities.
  • Integration: Combining new smart systems with legacy infrastructure can be technically complex.

But the future is promising. Emerging trends include:

  • Edge AI: Real-time processing at the source for ultra-low-latency response.
  • Digital twins: Simulating conveyor systems for diagnostics and optimization.
  • Reinforcement learning: Self-adjusting systems that learn to optimize over time.

These innovations will push AI-powered monitoring even further, toward autonomous, self-healing conveyor infrastructure.

Conclusion

AI is transforming conveyor belt monitoring from a manual, reactive task into a smart, automated system capable of real-time diagnostics, predictive maintenance, and performance optimization.

For mining and industrial operations, this means safer workplaces, fewer disruptions, and more profitable outcomes.

With AI technologies like machine learning, computer vision, and IoT working together, conveyor systems are no longer just moving materials, they’re generating insights that move entire industries forward.

Source Acknowledgment
This article is informed by insights from the academic review:
“Applications of Artificial Intelligence for Smart Conveyor Belt Monitoring Systems” by Murtadha Shukur Mahmood and Israa Rafie Shareef, published in Journal Européen des Systèmes Automatisés (JESA), Vol. 57, No. 4, August 2024. DOI: 10.18280/jesa.570426